Call: +27834270994
 Send Inquiry
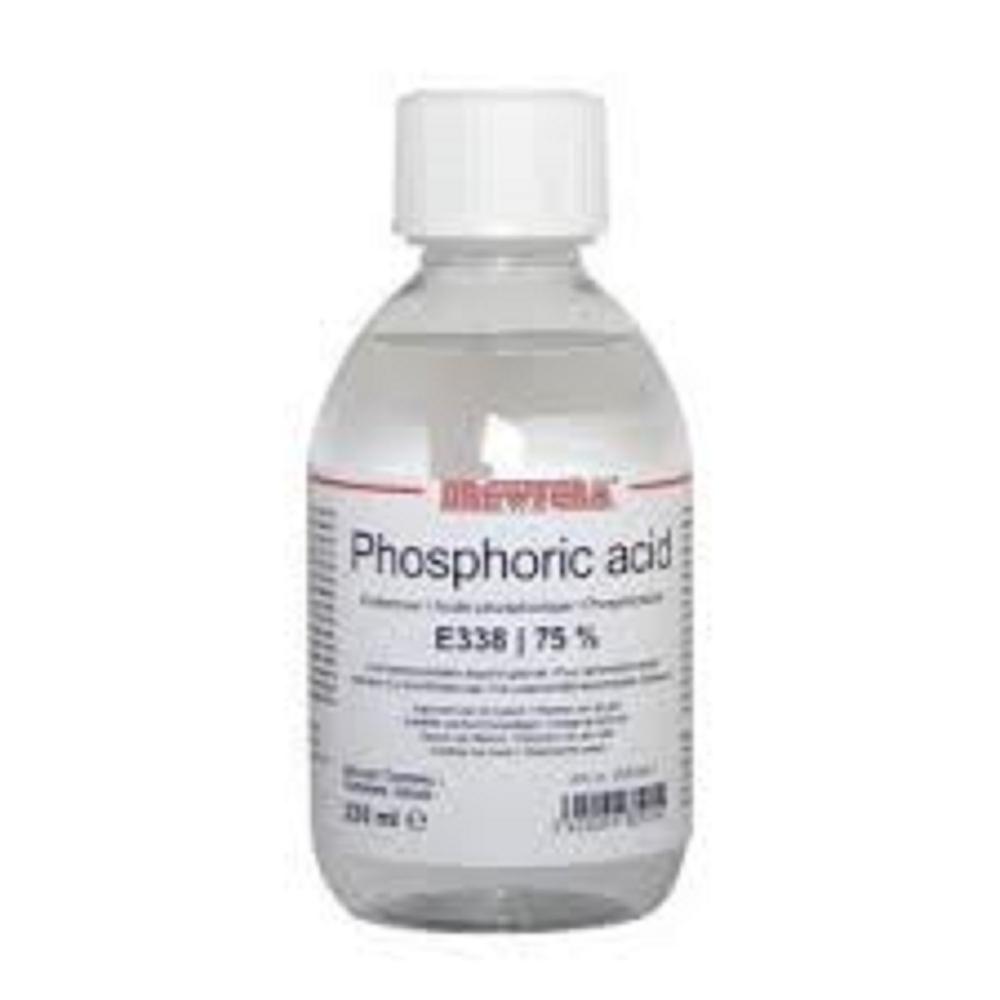
Phosphoric acid
85.0 USD ($)/Metric Ton
Product Details:
- Structural Formula H-O-P(=O)(OH)2
- Taste Sour, acidic
- Smell Odorless
- Molecular Formula H3PO4
- Refractive Rate nD 1.433 (75% solution)
- Boiling point 158C (decomposes)
- HS Code 28092090
- Click to View more
X
Phosphoric acid Price And Quantity
- 85.0 USD ($)/Metric Ton
- 50 Metric Ton
Phosphoric acid Product Specifications
- Orthophosphoric acid, E338
- Inorganic Acid
- 42.35C (pure form)
- Miscible with water
- 98.00 g/mol
- Acidifier in foods and beverages, rust inhibitor, dental etchant, fertilizer production, catalyst
- nD 1.433 (75% solution)
- Phosphoric Acid
- 7664-38-2
- H3PO4
- 75%
- Food Grade, Laboratory Grade, Industrial Grade
- H-O-P(=O)(OH)2
- Food industry additive, Laboratory use, Industrial use, Water treatment, Dentistry
- Sour, acidic
- Phosphate rock, Sulfuric acid
- 1.685 Gram per cubic centimeter(g/cm3)
- 28092090
- Clear colorless liquid
- 231-633-2
- Odorless
- 158C (decomposes)
- Plastic bottle
- Corrosive (Class 8)
- Non-flammable
- Wet Process, Thermal Process
- 2 years if stored properly
- 0.028 mmHg (at 20C)
- 250 ml
- Keep container tightly closed in a dry, cool, well-ventilated place
- Colorless
- Stable under recommended storage conditions
- 1.5
Phosphoric acid Trade Information
- South Africa
- Paypal, Days after Acceptance (DA), Delivery Point (DP)
- 50 Metric Ton Per Week
- 50 Week
Product Description
Phosphoric Acid is a versatile, high-performance inorganic acid used across industries including food & beverage, agriculture, pharmaceuticals, and industrial cleaning. Our high-purity phosphoric acid is available in food grade and industrial grade, offering a reliable solution for applications requiring precision, consistency, and safety.
In the food industry, phosphoric acid functions as a pH regulator, acidulant, and flavor enhancer, commonly used in soft drinks, jams, and processed foods. In industrial settings, it serves as an effective rust remover, metal surface treatment agent, and scale remover, making it indispensable in manufacturing and maintenance environments.
Produced under strict quality controls, our phosphoric acid guarantees high stability, consistent concentration, and compliance with global quality standards. Whether you're sourcing for formulation, production, or cleaning purposes, this multi-use acid delivers performance, purity, and value.
Versatile Applications Across Industries
Phosphoric acid serves as a vital ingredient in various industries, from food and beverages as an acidifier (E338) to laboratory reagents, water treatment chemicals, dental etchants, and rust inhibitors. Its consistent stability and high purity make it an ideal choice for multiple professional uses.
Safe Handling and Easy Storage
This 75% solution arrives in a durable 250 ml plastic bottle, designed to ensure safe handling. The acid is stable under recommended storage-cool, dry, well-ventilated conditions with the container tightly closed-ensuring both longevity and preservation of quality for up to two years.
High Purity and Quality Assurance
Manufactured through rigorous wet and thermal processes, our phosphoric acid offers high consistency and adherence to food, laboratory, and industrial grade requirements. Each batch is tested to ensure optimal purity and physical properties, making it suitable for sensitive and regulated environments.
FAQ's of Phosphoric acid:
Q: How should phosphoric acid be safely stored and handled?
A: Phosphoric acid should be stored in its original, tightly closed plastic bottle in a dry, cool, well-ventilated location. Always use personal protective equipment when handling, as it is a corrosive substance (Class 8). Avoid exposure to moisture and incompatible substances to maintain product stability.Q: What are the primary industrial applications of phosphoric acid?
A: Phosphoric acid is widely used as an acidifier in foods and beverages, a rust inhibitor, dental etchant, water treatment agent, catalyst in chemical processes, and for fertilizer production. Its versatility makes it a staple across manufacturing, laboratory, and processing industries.Q: When should phosphoric acid be replaced or disposed of?
A: Phosphoric acid retains optimal quality for up to two years when stored as recommended. Replace or dispose of any product that has surpassed its shelf life or shows signs of contamination, following proper hazardous waste regulations due to its corrosive nature.Q: Where is phosphoric acid commonly used within the food industry?
A: In the food industry, phosphoric acid is primarily utilized as an acidifier in the production of soft drinks, processed foods, and as an additive for pH regulation. Its clear, food-grade solution ensures safety and consistency for consumable products.Q: What is the production process for this phosphoric acid?
A: This phosphoric acid is produced via wet and thermal processes, starting with phosphate rock and sulfuric acid as raw materials. These methods ensure a high-purity and consistent final product suitable for demanding food, laboratory, and industrial applications.Q: How does using phosphoric acid benefit laboratory and industrial procedures?
A: Phosphoric acid's stable, high-purity formulation offers reliable pH control, excellent reactivity in analytical chemistry, and efficient rust inhibition. Its water miscibility and non-flammable nature enhance safety and operational convenience in laboratories and industrial settings.Tell us about your requirement

Price:
Quantity
Select Unit
- 50
- 100
- 200
- 250
- 500
- 1000+
Additional detail
Mobile number
Email

Other Products in 'Feed Preservation Acid' category

Contact Details
PAGE GLOBAL EXPORT (PTY) LTD.
- 1, Charles Street, Bloemfontein - 9301, Free State, South Africa
- Phone :+27--834270994

 Send Inquiry

Developed and Managed by Infocom Network Private Limited.
