Call: +27834270994
 Send Inquiry


Sorbic acid
75.0 USD ($)/Metric Ton
Product Details:
- Structural Formula CH3-CH=CH-CH=CH-COOH
- Boiling point Not applicable (decomposes)
- Taste Slightly acidic
- Molecular Formula C6H8O2
- HS Code 29161990
- Molecular Weight 112.13 g/mol
- Smell Odorless or faint characteristic
- Click to View more
X
Sorbic acid Price And Quantity
- 50 Metric Ton
- 75.0 USD ($)/Metric Ton
Sorbic acid Product Specifications
- Food preservative, pharmaceuticals, cosmetics, animal feed
- Antimicrobial agent to prevent growth of mold, yeast, and fungi in foods and beverages
- 99% min
- CH3-CH=CH-CH=CH-COOH
- 1.204 Gram per cubic centimeter(g/cm3)
- 110-44-1
- 2,4-Hexadienoic acid
- 112.13 g/mol
- 203-768-7
- Derived from crotonaldehyde and ketene
- 29161990
- C6H8O2
- Slightly acidic
- Sorbic Acid
- 132 C
- Not applicable (decomposes)
- Organic Acid
- Odorless or faint characteristic
- Food grade, Pharma grade
- Slightly soluble in water, soluble in ethanol and ether
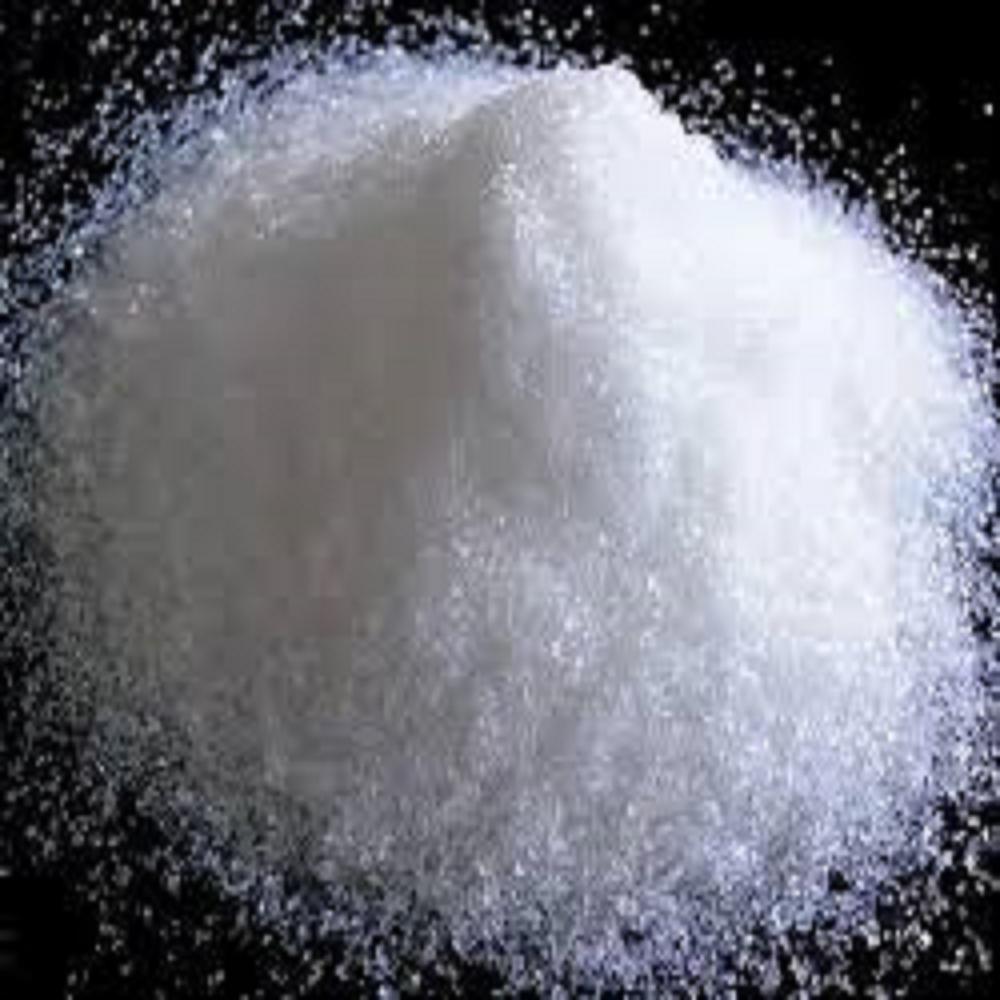
- White crystalline powder or granules
- Pathogenic bacteria absent
- 99.0%
- 0.5%
- 10 ppm
- 3.5 - 4.5
- 3 ppm
- 2 ppm
- 25 kg fiber drum or bag, customized packaging available
- 24 months in unopened packaging
- Store in a cool, dry, well-ventilated area, away from sunlight and moisture
Sorbic acid Trade Information
- South Africa
- Paypal, Days after Acceptance (DA), Delivery Point (DP)
- 50 Metric Ton Per Week
- 50 Week
Product Description
Maintain freshness and extend shelf life naturally with our high-purity Sorbic Acid, a widely trusted food-grade preservative ideal for preventing mold, yeast, and fungal growth. Recognized for its effectiveness and safety, Sorbic Acid is used across a broad range of applications, including baked goods, cheeses, beverages, personal care products, and more.
Produced to strict industry standards, our Sorbic Acid offers superior performance with minimal taste impact, making it a preferred solution for manufacturers seeking clean, efficient, and cost-effective preservation. With its excellent solubility and compatibility with other ingredients, it ensures product integrity and stabilityboosting consumer confidence and reducing spoilage-related losses.
Whether you're in food production, cosmetics, or pharmaceuticals, our Sorbic Acid powder delivers consistent results backed by purity, quality, and regulatory compliance.
Wide-Ranging Applications
Sorbic acid serves as a versatile antimicrobial agent, essential in the food industry for preserving freshness and extending shelf life. It also finds use in pharmaceuticals, cosmetics, and animal feed, thanks to its efficacy against molds and yeasts without altering the taste or odor of products.
Quality and Safety Assured
With a purity of at least 99%, sorbic acid meets stringent quality standards. Its microbiological safety is confirmed, as pathogenic bacteria are absent, and heavy metal content is kept to a minimum (lead: 2 ppm, arsenic: 3 ppm). It is tested for loss on drying, maintaining no more than 0.5% moisture content for consistent performance.
Packaging and Storage Recommendations
Packaged in robust 25 kg fiber drums or bags, with options for customized packaging to suit different needs, sorbic acid maintains its stability and efficacy. For optimal shelf life and quality, store in a cool, dry, and well-ventilated area, away from direct sunlight and moisture.
FAQ's of Sorbic acid:
Q: How should sorbic acid be stored to ensure maximum shelf life?
A: Store sorbic acid in a cool, dry, and well-ventilated area, keeping it away from sunlight and moisture. Proper storage conditions help maintain its stability and extend its shelf life to up to 2 years.Q: What is the recommended usage of sorbic acid in the food industry?
A: Sorbic acid is used as an antimicrobial preservative to prevent the growth of mold, yeast, and fungi in various foods and beverages. It ensures extended freshness without affecting the product's flavor or aroma.Q: Where does sorbic acid find applications beyond food preservation?
A: Apart from food, sorbic acid is also applied in pharmaceuticals, cosmetics, and animal feed as a preservative, leveraging its antimicrobial and non-reactive properties.Q: What are the benefits of using sorbic acid as a preservative?
A: Sorbic acid effectively inhibits spoilage organisms, prolongs shelf life, and maintains product safety. Its low toxicity, odorless nature, and negligible impact on taste make it ideal for sensitive applications.Q: What packaging options are available for sorbic acid, and can they be customized?
A: Sorbic acid is typically supplied in 25 kg fiber drums or bags. Packaging can be customized according to specific requirements, offering flexibility for different distribution or storage needs.Q: How is sorbic acid produced and what is its purity level?
A: Sorbic acid is synthesized from crotonaldehyde and ketene, resulting in a highly pure product (minimum 99% on dry basis), suitable for both food and pharmaceutical applications.Q: When should sorbic acid be used in manufacturing processes?
A: Sorbic acid should be added during production or packaging to ensure comprehensive preservation throughout the product's shelf life, preventing microbial contamination effectively.Tell us about your requirement

Price:
Quantity
Select Unit
- 50
- 100
- 200
- 250
- 500
- 1000+
Additional detail
Mobile number
Email

Other Products in 'Feed Preservation Acid' category



Contact Details
PAGE GLOBAL EXPORT (PTY) LTD.
- 1, Charles Street, Bloemfontein - 9301, Free State, South Africa
- Phone :+27--834270994

 Send Inquiry

Developed and Managed by Infocom Network Private Limited.
